Inside an M12 Connector Factory: Precision Manufacturing for Industrial Reliability
2026-11-16
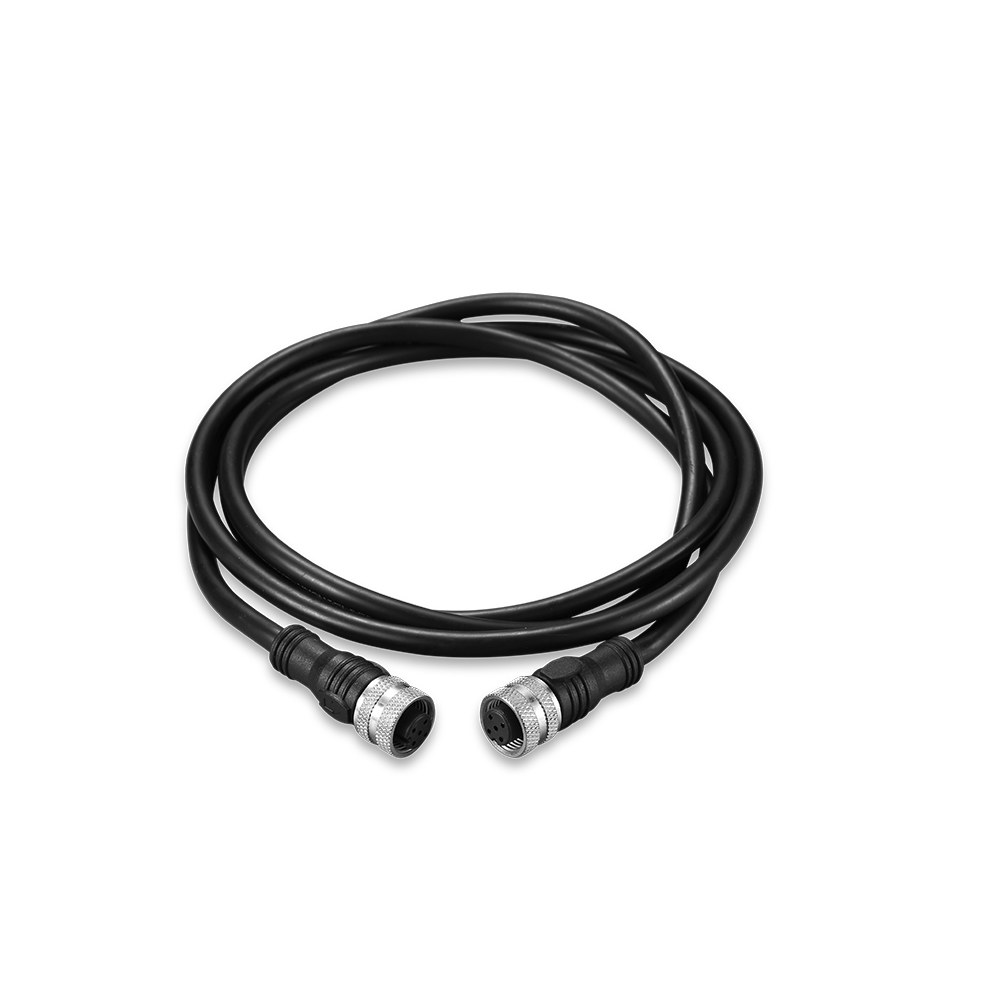
When a single connection failure can halt an entire production line, the humble M12 connector becomes anything but ordinary. Inside an REUNION factory, we saw firsthand how microscopic precision and obsessive testing turn these compact components into unshakeable links in industrial automation. It’s a world where every micron matters, and reliability isn't just a promise—it's built in, layer by layer. Here’s a rare look behind the scenes.
Bronze and brass enter, reliability exits
When bronze and brass components are introduced into critical systems, the promise of reliability quickly fades. These materials may look timeless, but their mechanical properties betray that elegance. Under cyclic loads or subtle vibrations, work hardening turns ductile brass brittle, setting the stage for sudden fracture. Bronze, for all its corrosion-resistant reputation, often brings a hidden penalty: unpredictable friction coefficients that wear down mating parts and invite galling. The very things that once made these alloys attractive—easy formability, a patina of tradition—now become liabilities when consistent performance is non-negotiable.
In practice, the presence of bronze and brass in a design is an open invitation to maintenance. Threaded brass fittings in fluid systems, for example, are notorious for seizing under thermal expansion, making routine disassembly a battle. Valve seats in bronze slowly erode, altering flow characteristics in ways that no sensor catches until the process drifts out of spec. Engineers who inherit legacy equipment often trace unexplained downtime to a single brass bushing that chose to deform rather than slide, or a bronze worm gear that sacrificed itself to misalignment. The pattern is stubborn: as soon as these metals enter, the system’s dependable rhythm walks out the door.
The alternative is unglamorous but honest. Where bronze and brass exit the bill of materials, you find polymers that damp vibration without hardening, stainless alloys that disregard corrosion without the friction penalty, or even plain steel where coatings do the protective work. It’s not about chasing novelty; it’s about recognizing that reliability lives in materials that refuse to surprise you. Drop the bronze, spec a material that cares only about consistent behavior, and watch unplanned shutdowns become just another forgotten statistic.
Inside the silent choreography of automated lines
There’s no barked command, no shouted countdown, just the soft hiss of pneumatics and the whisper of conveyor belts sliding into position. Each robotic arm swings into its arc with the precision of a dancer who has rehearsed the same movement a million times—because in a sense, it has. Sensors read invisible cues in the air, guiding grippers to the exact millimeter, while cameras blink in rapid-fire bursts, checking angles, alignment, speed. It’s a performance unspooling for an audience of none, yet every beat matters.
The strangeness of this dance lies in its absolute consistency. A human choreographer might relish impromptu flourishes, but here, variation is the enemy. Pallets drop, components marry together, labels glide onto packages with a rhythm so steady it begins to feel like a heartbeat—only it’s a heartbeat that never quickens with excitement and never misses a pulse. In that stillness, a different kind of beauty emerges: the elegance of pure function, stripped of ego and fatigue.
Even the silences are choreographed. A pause of exactly 0.8 seconds allows adhesive to cure before the next part arrives. Two seconds of stillness let a thermal camera confirm a seal’s integrity. These deliberate rests, invisible to the untrained eye, form the hidden grammar of the line. Watching long enough, you start to read it not as machinery but as a quiet conversation—a sequence of unspoken agreements between steel and software, looping endlessly into the hum of production.
A microscopic view of the crimp that never lets go
Peering through the lens, the crimp reveals itself not as a simple wave but as a labyrinth of interlocking bends where each fiber seems to memorize its neighbor’s curve. The structure is almost organic, like a fingerprint pressed into the material at birth, refusing to straighten even under tension. You can see where stress concentrates at the apex of each zigzag, yet the crimp holds—its resilience is less about strength and more about a distributed stubbornness, a collective refusal of the strands to forget their original shape.
At ten thousand times magnification, the surface becomes a landscape of micro-kinks and asymmetrical ridges that lock together like dry stone walls. There’s no adhesive, no chemical bond forcing them to stay; it’s purely geometry at war with entropy. The crimp persists because any force that tries to flatten it gets tangled in a cascade of tiny misalignments, each one a trapdoor for energy. It’s a slow, patient mechanism—the kind that laughs at the idea of permanent deformation.
What’s astonishing is how this random-looking tangle actually follows a hidden order, a fractal-like repetition of loops within loops. The crimp never lets go because it was never a single event to begin with; it’s a memory of all the stresses, twists, and thermal dances the fiber endured during its formation. Under the microscope, it’s a quiet monument to the idea that some things are held together not by force, but by the sheer tenacity of their own history.
Baking, freezing, drowning: the lab where connectors earn their keep
Inside the test lab, connectors are punished with a kind of grim creativity. Thermal chambers crank up past boiling point, then plunge deep into sub-zero chill within minutes, cycling hundreds of times until materials crack or seals surrender. It’s not enough to survive one extreme; the real failure comes in the transition, where expanding metals and shrinking plastics fight each other until something gives. Technicians listen for the faint click of a contact letting go, or watch for the fog of condensation that means moisture has found a way in.
Then there’s the water—not a polite spray, but full immersion in salt-laced tanks, sometimes while the connector carries high voltage. It’s a slow-motion drowning where corrosion creeps along pins, searching for microscopic gaps in plating. Other specimens lie baking under ultraviolet lamps, their polymer housings turning chalky and brittle over weeks, simulating years on a sun-scorched engine deck. The lab is a gallery of controlled destruction, and every scar tells the engineers what needs to be redesigned.
What earns a connector its place in the real world isn’t just passing these trials, but failing predictably. Boundaries are mapped with exquisite precision: the exact number of thermal shocks before delamination, the precise salinity that starts eating through gold plate, the vibration frequency that unseats a crimp. This violent curriculum turns newcomers into battle-hardened parts, carrying the memory of every torture chamber they survived. By the time they ship, they’ve already endured far worse than most installations will ever throw at them.
When the catalog ends and true engineering begins
There’s a quiet moment in every project when the familiar pages of supplier catalogs no longer offer what you need. The off-the-shelf hinge is a few millimeters too tall, the listed load rating doesn’t account for that off-axis force, the material spec is close but not quite right for the chemical washdown. That’s where the real work starts. You stop browsing and start calculating. You take stock of the actual constraints—temperature swings, vibration spectra, fit tolerances nobody thought about in the initial design review—and you realize the component you were looking for doesn’t exist yet. It has to be made.
Engineering first principles come back into focus: stress distributions, fatigue life, galvanic compatibility, manufacturing feasibility. You sketch a custom bracket on a notepad, run a quick FEA study over lunch, and by afternoon you’re emailing a small fabrication shop that can machine it from a solid billet instead of welding three catalog parts together. The solution ends up lighter, stronger, and oddly cheaper once you factor in assembly time. This shift in mindset—from searching for a part number to defining a function and designing backward from failure modes—is what separates assembling from engineering. It’s not about rejecting catalogs entirely; it’s about recognizing their margins. The best designs often live just past the last page.
The human eye and laser beam that sign off every single part
There’s something quietly remarkable about the moment a finished component passes its final check. It isn’t just another item rolling off the line; it’s a piece that has survived every tolerance, every thermal cycle, every vibration test. The last pair of eyes to study it – often those of a veteran inspector – catches flecks of irregularity that no automated system has yet learned to name. A tiny discolorations, a whisper of porosity, the ghost of a tool mark: these are the details that decades of hands-on work teach someone to distrust. That human glance, half instinct and half hard-earned pattern recognition, is still the first true signature of quality.
But the eye doesn’t work alone. Right beside it, a precisely calibrated laser beam sweeps the same surface, measuring parameters we can’t feel. It chases micron-level contours, reflects off edges, and compares what it sees to a digital twin that knows exactly how the part should exist in three dimensions. Where the inspector’s gaze brings intuition, the laser brings unforgiving mathematics. Together they form a strange partnership: the warm, learned judgment of a person and the cold, absolute verdict of light. One can overthink; the other cannot think at all. And yet, when they agree, the part is released – silently authorized by two very different kinds of attention.
This double sign-off isn’t a checkbox. It’s a ritual that factory floors rarely advertise. The human eye might catch a burr the laser was never programmed to look for; the laser might reveal a deviation the eye would confidently overlook. Neither is perfect, but their overlap creates a safety net woven from both craft and physics. Every single part that leaves the building carries the memory of that last combined scrutiny – a final stamp of approval that no single sensor, no single mind, could ever reproduce alone.
FAQ
Most M12 connectors use gold-plated brass or phosphor bronze for the contacts to ensure low contact resistance and strong corrosion resistance. The housings are often nickel-plated brass, stainless steel, or ruggedized plastic like PA66, depending on whether the application needs EMI shielding, chemical resistance, or lightweighting. The choice isn't just about conductivity; it's about surviving vibration, humidity, and aggressive fluids without signal loss over years in the field.
It starts with vision-guided pick-and-place systems that align pins to within fractions of a millimeter, combined with laser height sensors that verify seat depth before crimping. The real precision comes from real-time force monitoring during termination—machines reject any crimp that falls outside the specified compression curve, which catches inconsistencies that human eyes would miss. After molding or screwing on the body, a final optical inspection scans thread geometry and pin position to ensure the connector will mate perfectly every time.
Every batch goes through a gauntlet—contact resistance measurements, high-potential dielectric tests to check insulation, and pulsed thermal cycling to simulate years of temperature swings. But the telling test is the 100% continuity check under lateral load: the cable is bent at a right angle near the strain relief while the system watches for microsecond-level opens. That’s where you catch latent assembly faults that would only show up after installation in a vibrating machine frame.
Overmolding isn't just adding a rubber boot. It's a chemical bonding process where the molten TPE or PUR must fuse to the cable jacket and the connector body without introducing voids. If the mold temperature or injection speed is off, you get microscopic gaps that pass a quick pressure test but fail after thermal cycling. Factories spend a lot of time fine-tuning the gate location and holding pressure so the seal behaves like a single homogeneous part, not a layered assembly that can delaminate.
They use colour-coded insert tooling and software-controlled terminal placement machines that read the coding from the production order and load the correct pin pattern without human changeover. The real challenge is in testing: a universal test fixture automatically switches between sensor, data, and power pin layouts so that a D-coded connector doesn't get tested against an A-coded spec. Batch tracking is done via laser-etched QR codes that follow the connector through every station, preventing mixing.
In the crimping and plating areas, the air is filtered to a controlled level because even a speck of dust on a gold-plated pin can create a micro-pit that corrodes under humidity. Operators wear electrostatic-safe garments, and everything—from the transport trays to the cutting blades—undergoes regular particle count checks. It's not about making it look clean; it's about preventing a 50-micron particle from becoming the start of a creep path that eventually causes a field failure.
They use mixed-flow corrosion chambers that pump in dilute sulfur dioxide and hydrogen sulfide while cycling temperature and humidity—much harsher than a typical salt spray test. UV exposure is done with xenon arc lamps that mimic sunlight spectrum, and vibration profiles are recorded from actual diesel generators or robotic arms so the test bench replicates the same resonances. A connector isn't signed off until it survives 1,000 hours of combined stress and still shows a contact resistance drift of less than 1 milliohm.
Conclusion
Walk into the M12 connector factory and the first thing you notice is how raw bronze and brass stock seem to vanish into one end while finished, unforgivingly reliable connectors emerge from the other. It is less a linear process and more a quiet transformation orchestrated by automated lines that hum with a kind of silent choreography. Robots and precision tools move in lockstep, stripping wire, positioning contacts, and executing high-force crimps that, when viewed under a microscope, reveal gas-tight cold welds that never let go—the atomic-level bond that makes intermittent failures almost unthinkable. Every connector then journeys into a chamber of extremes: a lab where they are cycled through blistering heat, subzero cold, and hours of pressurized immersion. This ritual of baking, freezing, and drowning is not a suggestion; it is the price of admission to environments where salt spray and vibration are the default.
Yet what truly separates a commodity from a purpose-built connector happens when the standard catalog no longer fits. Real engineering begins in conversations about custom pin layouts, specialized over-molding, or shielding against a particular industrial noise profile. Once a design is frozen, the factory pivots from batch automation to one-piece flow, where every single part is inspected with a human eye and a laser beam in parallel. The operator looks for subtle burrs or plating inconsistencies while an optical profilometer measures critical dimensions down to micrometers. Only then does the connector earn its mark, ready to disappear inside a machine tool, a food-processing line, or a rail signal system—quietly delivering the industrial reliability it was forged to provide.
Contact Us
Contact Person: Hayley Liang
Email: [email protected]
Tel/WhatsApp: +86 13480625451
Website: https://www.reunion-china.com/