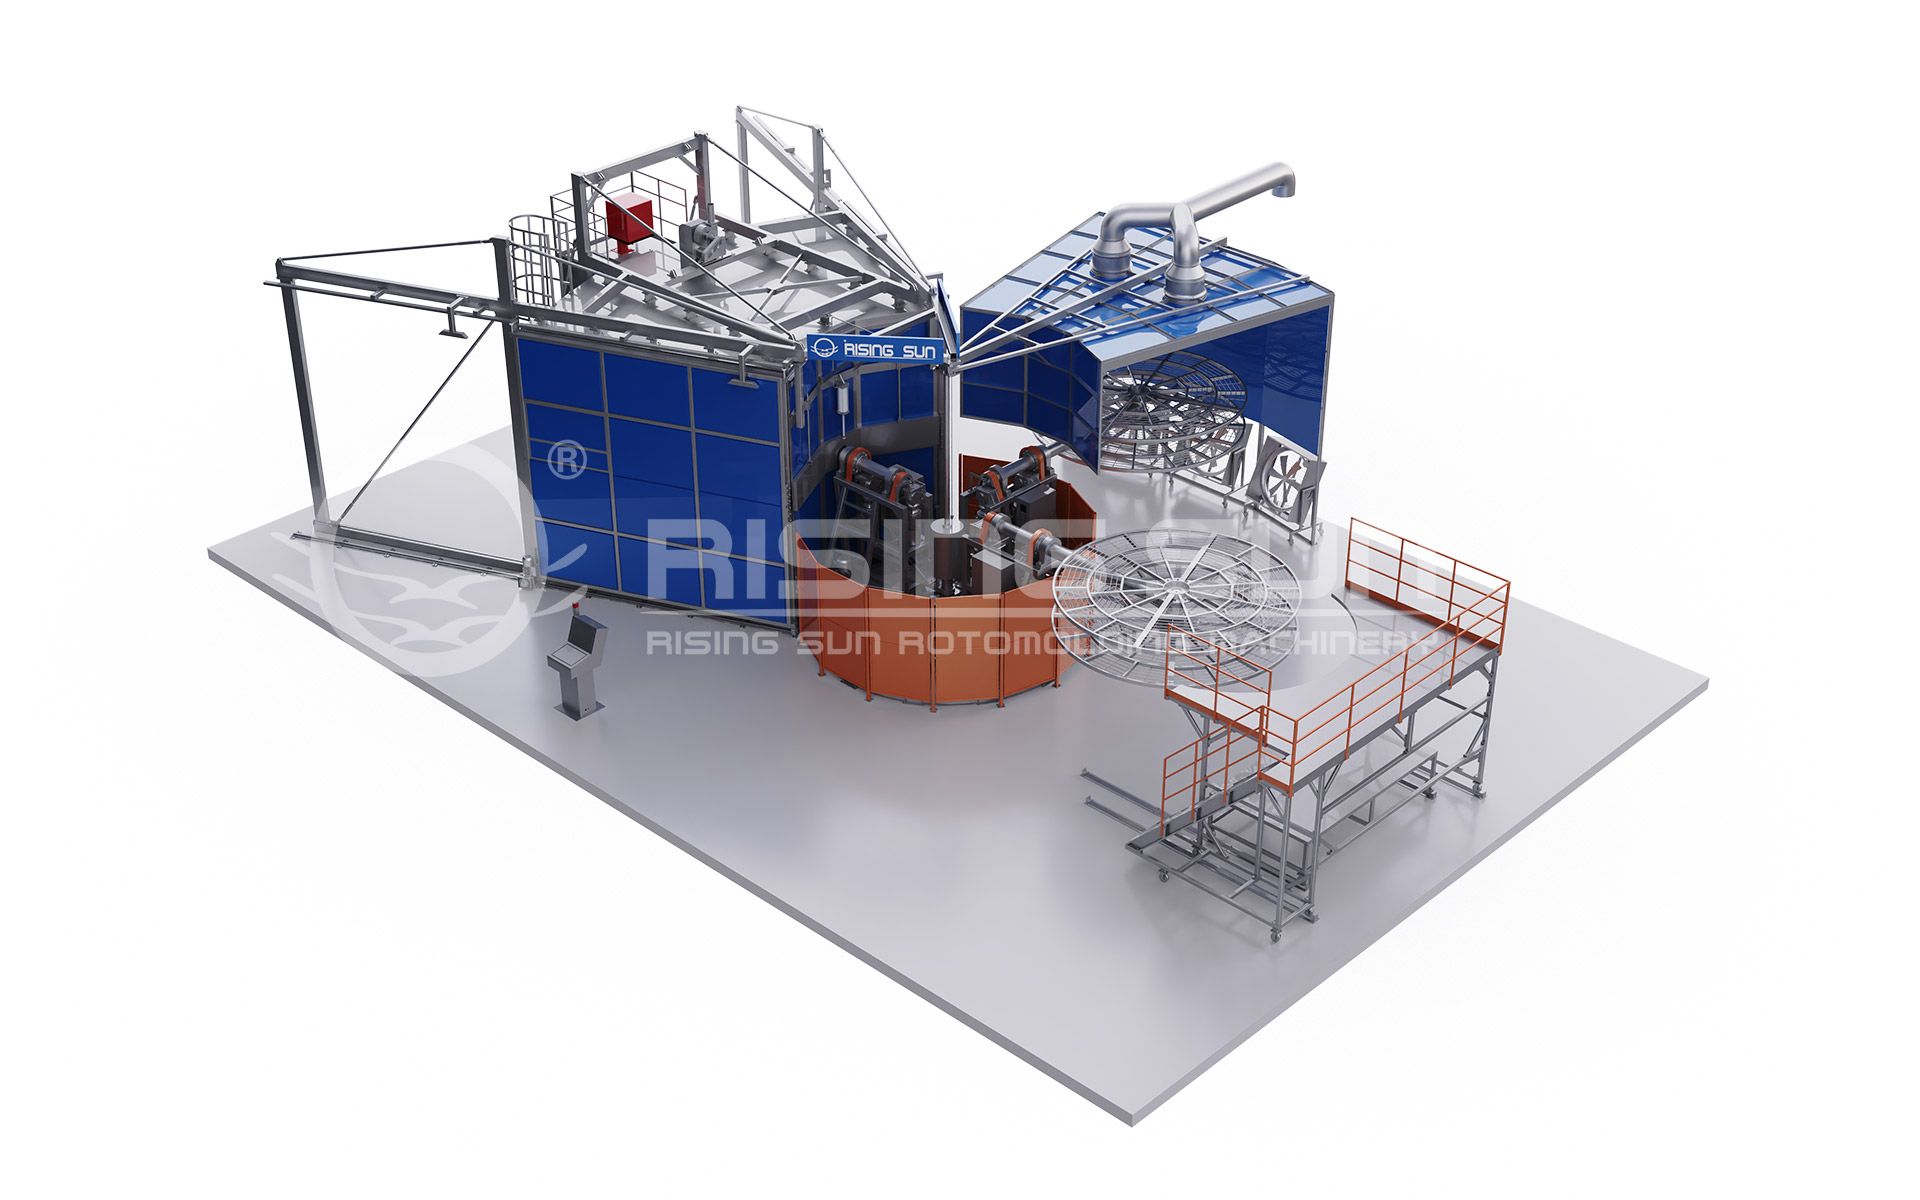
Stationary Oven Carousel Rotomolding Machine Company: Key Factors for Selecting a Reliable Manufacturer
2026-09-30
Rotomolding lines live or die by the oven carousel. Before you sign with a manufacturer, ask yourself: will they still answer the phone in year five? In this guide, we look past glossy brochures at the factors that actually predict long-term reliability—drawing on what Rising Sun has learned from real production floors. It’s the kind of pre-purchase thinking that saves you from costly downtime later.
How Long Has the Manufacturer Been Building Stationary Oven Carousels?
A manufacturer's tenure in building stationary oven carousels often reveals more than just a number—it signals a deep familiarity with the quirks of thermal cycling, load distribution, and the wear points that only emerge after years of continuous operation. Some workshops have been refining these systems since the early 1990s, when the shift from manual batch ovens to automated horizontal carousels first gained traction in industrial bakeries. That kind of longevity isn't about bragging rights; it means the design has been quietly adjusted through hundreds of real-world baking seasons, from humidity-related bearing swaps to chain tension fixes that never make it into a brochure.
You might not find a single "founding date" plaque on the factory floor, but the evidence shows up in the details: serial numbers that trace back to early prototype runs, legacy mounting brackets still compatible with newer drives, and service teams who can troubleshoot a 20-year-old unit from memory. Builders who've been at this for three decades tend to accumulate a library of niche solutions—like oversized sprockets for sticky dough environments or corrosion-resistant trunnions for high-acid marinade lines. Those refinements don't come from a spec sheet; they come from watching carousels run past their warranty periods and learning what actually fails.
When comparing manufacturers, ask for a production timeline or a list of the oldest still-operating units they've built. If a company has been turning out stationary oven carousels since before digital controls became standard, they've likely managed the messy transition from relay logic to PLC-driven indexing without losing the mechanical backbone that keeps everything rotating true. Longevity in this niche isn't just about surviving; it's about the iterative, unglamorous grind of making a circular oven platform that doesn't wobble after 50,000 cycles.
Why Oven Insulation and Airflow Deserve More Attention
Most home cooks obsess over racks and temperature dials, yet the real unevenness in baking often traces back to thin, degraded insulation or a poorly designed air path. When heat escapes through weak seals or dead spots starve the fan, the oven cycles harder and still leaves cold corners. That’s why two identical recipes can come out so differently in the same model year after year.
Airflow gets even less credit. A convection fan that pushes air sideways instead of swirling it around the cavity will dry out the leading edge of a tray of cookies while the back row stays pale. If the venting is too aggressive, moisture leaves before bread sets; too weak, and roast vegetables steam instead of brown. Paying attention to how air moves through your particular oven beats adding another thermometer.
The payoff is immediate once you stop treating insulation and airflow as afterthoughts. You’ll notice shorter preheat times, quieter operation, and fewer burnt edges on dense bakes. Small fixes like replacing a worn door gasket or repositioning a warped baffle can outperform a new appliance.
Evaluating Carousel Load Capacity and Balance for Consistent Rotation
Before adding items to any rotating carousel, confirm the total expected weight stays below the manufacturer’s listed limit for the central bearing and drive gear. Uneven placement causes more trouble than raw weight alone: a heavy item on one side forces the motor to work harder through part of each revolution and can accelerate wear on chain links or rollers. Measure the distance from the spindle to the heaviest loads, and keep the moment roughly equal on opposite sides rather than relying on a simple pound total.
Run the carousel slowly after loading and listen for rhythmic hesitation or slight speed changes. Those changes often signal a balance issue that will grow worse under continuous operation. Small counterweights or repositioning can correct much of the problem, but avoid adding weight in ways that overload one bearing or create new friction points on the frame.
Periodic checks matter because fasteners can loosen as imbalance transfers force into the structure. Mark the starting position, rotate through several full cycles, and see whether the same point consistently drifts or sticks. If it does, inspect leveling feet, carrier alignment, and bearing play before increasing load or run time.
Mold Changeover Time and Tooling Flexibility on Fixed-Arm Systems
Trimming minutes off a mold change on a fixed-arm system rarely comes from a single dramatic fix. It usually starts with the small, unglamorous stuff—standardizing clamp heights, pre-staging bolts and fittings, and making sure the arm’s reach envelope isn’t forcing operators into awkward contortions just to reach a locating pin. When every second of downtime counts, a well-designed fixed-arm setup can drop changeover from hours to under fifteen minutes, but only if the mounting interface is thought through from the operator’s side of the machine.
Tooling flexibility on these systems often matters more than raw speed. A fixed arm doesn’t have to mean a fixed mindset: quick-change plates, magnetic clamping, and modular end-of-arm tooling let the same cell handle inserts, overmolding, or entirely different part families without re-engineering the whole station. The trick is designing the arm’s mounting face so that new tooling drops into the same kinematic location every time—no shimming, no guesswork. That repeatability is what turns a rigid structure into a genuinely flexible asset.
In practice, the biggest wins come from separating internal and external changeover tasks. Anything that can be done while the machine is still running—preheating a mold, staging the next tool cart, verifying air and water connections—should never wait until the old mold is out. On fixed-arm systems, adding a few well-placed quick disconnects and a visual guide for hose routing can shave off more time than a full automation retrofit. It’s not about making the arm faster; it’s about making the people around it less likely to waste motion.
What Spare Parts Availability Really Means for Production Uptime
Spare parts availability is not just about having a warehouse full of boxes. It determines how quickly a line can recover when something breaks. If a critical sensor or drive fails and the replacement is three days away, the entire shift plan collapses. The difference between a two-hour stop and a two-day stop rarely comes from the complexity of the repair—it comes from whether the part is within reach.
Many plants confuse inventory value with readiness. A shelf packed with low-turnover items can look reassuring while the parts that fail most often are missing. Tracking actual consumption patterns and linking them to maintenance records reveals which components deserve a local buffer. That kind of targeted availability protects throughput far better than a blanket increase in stock.
Production uptime also depends on supplier response, not just internal shelves. A vendor who can deliver overnight from a regional hub changes the math for expensive, rarely used items. So the real question is not "do we have spares?" but "how fast can we restore normal flow?" Answering that honestly shows what spare parts availability actually contributes.
Verifying Customer References and Real-World Machine Performance
Talking to existing users often reveals what spec sheets cannot. Ask for references from operations similar to yours in terms of materials, batch sizes, and duty cycles. When you call them, skip the general “are you happy?” question and instead probe for specifics: how often the machine needed unplanned maintenance in the first six months, whether the actual throughput matched the quoted figures once real-world variability kicked in, and how responsive the vendor was when issues did arise. A reference who hesitates or only offers vague praise is almost as informative as one who complains openly.
If possible, arrange a site visit to see the machine running a production job, not just a canned demonstration. Watch how the operators interact with it—do they trust the controls, or are there workarounds taped to the frame? Note the noise level, the ease of clearing jams, and whether the surrounding area is clean or littered with rejected parts. These details tell you more about long-term reliability than any brochure graph. Also ask about wear items: what has been replaced so far, at what hour count, and whether spare parts arrived quickly or sat in customs.
Finally, compare the vendor’s claimed uptime against the reference’s maintenance logs if they are willing to share them. Real-world performance is rarely linear; it degrades with ambient temperature swings, operator turnover, and inconsistent raw material quality. A machine that holds tolerance in an air-conditioned showroom may drift after three shifts in a hot, dusty plant. So when you evaluate references, focus less on the peak output number and more on the variance—how consistently the machine meets spec over hundreds of hours, and how gracefully it fails when pushed past its comfort zone.
FAQ
Start with the installed base in your specific industry. Ask for references from companies running the same oven size and similar part geometry, then find out how those machines handle temperature control zones and arm indexing over long production runs.
Request a list of machines that have been running for at least five years in your region. Contact those operators directly and ask about downtime patterns, maintenance logs, and how quickly the manufacturer resolved issues after commissioning.
Focus on oven air flow uniformity, the number of independent heating zones, carousel indexing accuracy, cooling station design, and whether the control system lets you store and recall recipes without reprogramming every run.
A lower upfront cost can hide weak service response times, limited spare parts inventory, and no remote diagnostics. When the machine stops, every hour of downtime usually costs more than the price difference between a good and bad supplier.
If you plan to run materials beyond standard polyethylene, such as nylon, PVC plastisol, or foamed resins, the manufacturer needs proven experience with different mold release systems, heating curves, and venting strategies. Not every oven design handles those equally well.
Good mold design means even wall thickness, proper vent placement, and no trapped air pockets. A manufacturer with in-house mold engineering can catch design flaws before you spend money on tooling, saving both time and scrap.
Look beyond the purchase price. Compare energy consumption per cycle, spare parts cost and availability, expected arm bearing life, and how often oven seals need replacement. Those numbers often reveal a very different long-term picture than the initial quote.
A visit shows you how they assemble frames, whether they test machines before shipping, and how they manage quality control. If a manufacturer hesitates to host you or limits access to certain areas, treat that as a serious red flag.
Conclusion
When narrowing down suppliers of stationary oven carousel rotomolding machines, the manufacturer’s track record often tells you more than a polished brochure. A builder with many years focused on fixed-arm carousel systems has usually learned the hard way where heat loss occurs, why balanced airflow matters inside the oven, and how uneven carousel loading can shorten bearing life. Ask about the insulation materials and the pattern of air circulation—these details directly affect cycle consistency and energy cost, yet they rarely appear in basic spec sheets. Similarly, pay close attention to the carousel’s load rating and how the arms are balanced for the molds you plan to run. A machine that struggles with your heaviest mold from day one will never deliver steady rotation or repeatable wall thickness.
Beyond the oven itself, consider how quickly molds can be changed on a fixed-arm system and whether the tooling setup allows for future mold sizes without major retrofits. Slow changeovers quietly eat into production capacity, no matter how good the heating looks. Spare parts availability is another area where a low purchase price can hide expensive downtime; a manufacturer with regional stock or fast shipping for wear items keeps your line moving when a drive component fails. Finally, take the time to verify customer references in similar applications, not just read case studies. Speaking with operators who run the same machine model daily reveals real-world performance, service responsiveness, and long-term reliability far better than any sales presentation can.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com