Stationary Oven Carousel Rotomolding Machine Maker: How to Choose the Right Partner for Your Production Line
2026-09-29
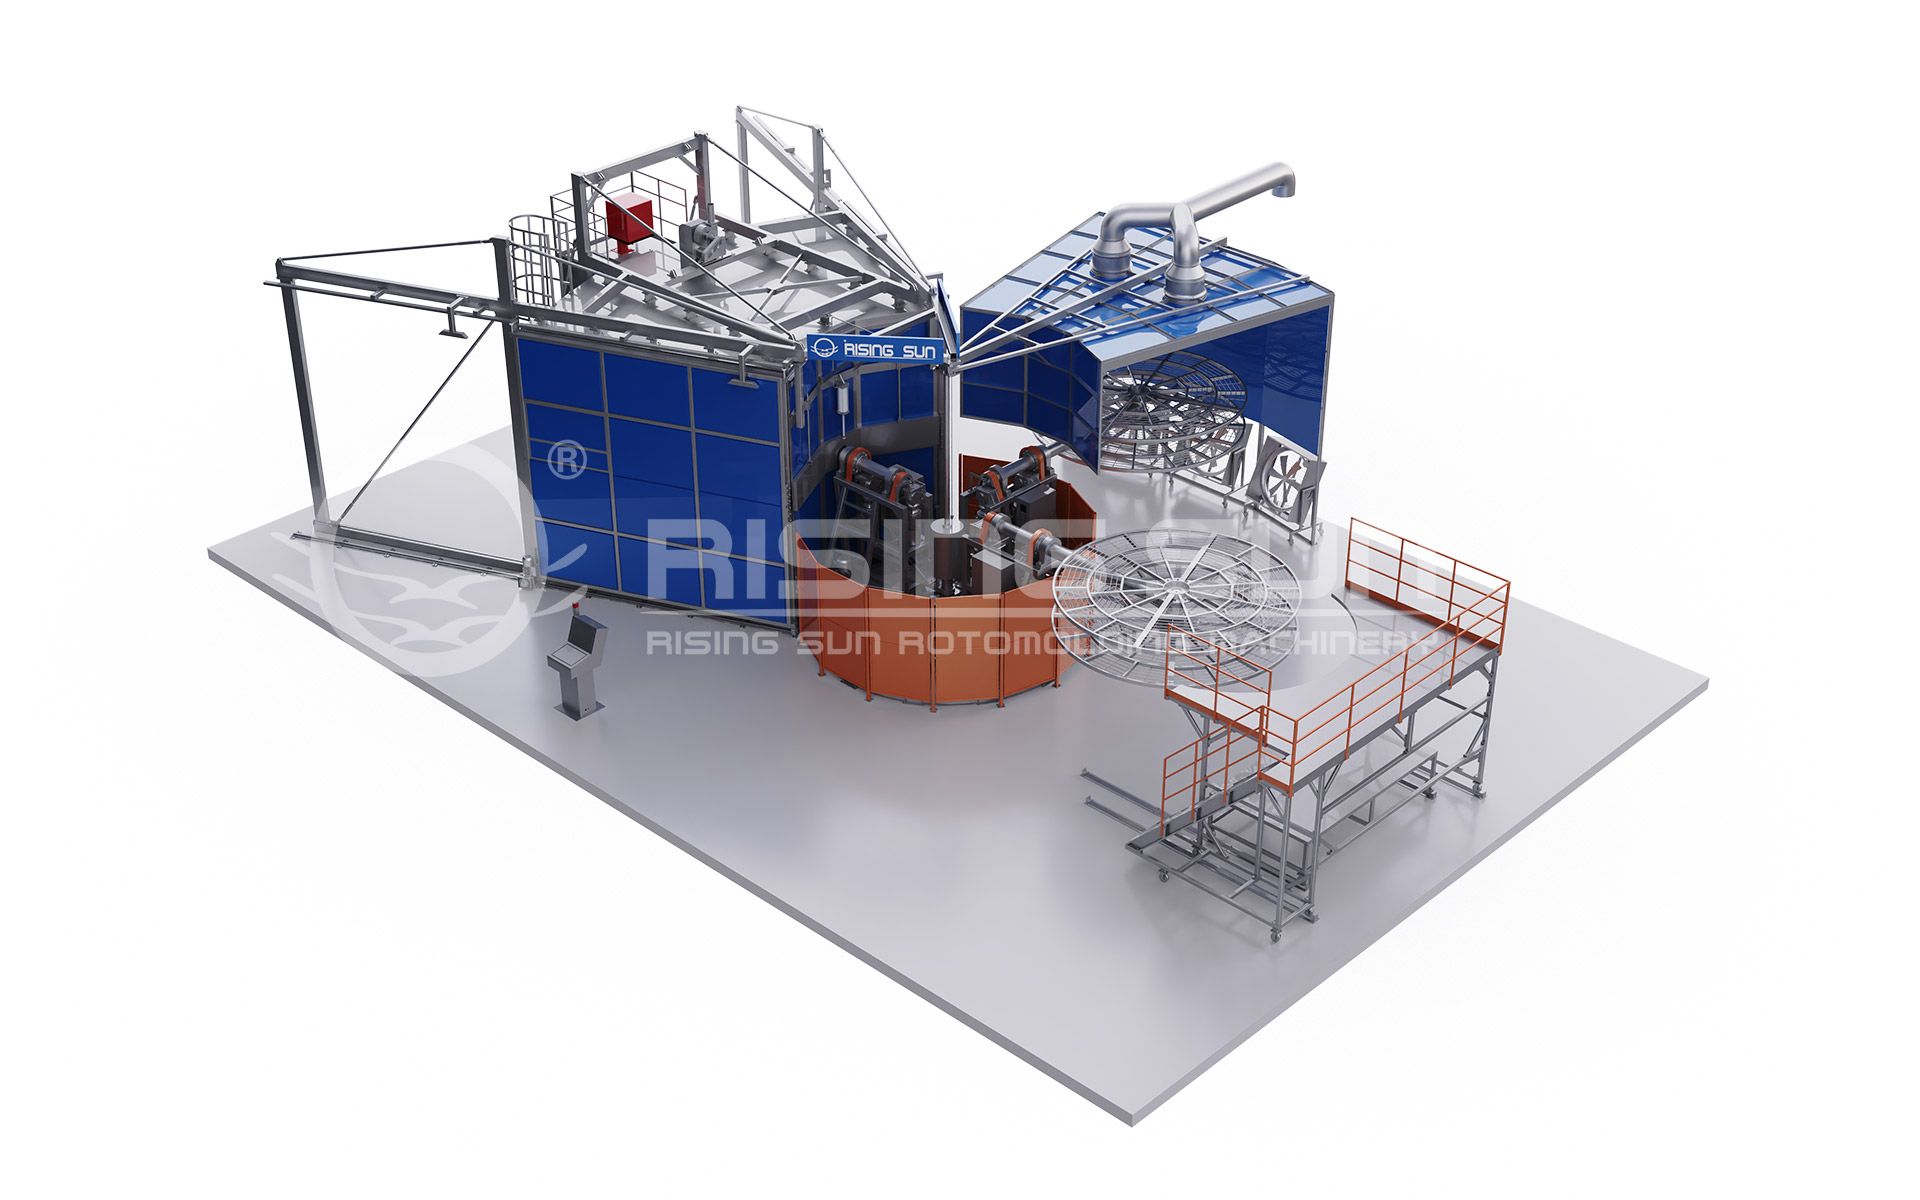
Your production line is only as strong as the rotomolding machine at its core—and the maker behind it. Choosing a stationary oven carousel machine partner isn’t a box-ticking exercise; it’s a decision that shapes your throughput, part quality, and maintenance burden for years. Rising Sun has spent years refining what that partnership should look like. Before you sign anything, here’s how to separate a true production ally from a mere equipment vendor.
Why a Maker's Floor Record Says More Than Their Sales Pitch
Sales pitch is a carefully curated story, but the floor record is the unedited diary. It shows what happened when the material arrived late, when the machine drifted out of tolerance mid-run, when an operator flagged a surface finish issue at 2 a.m. Those handwritten corrections, timestamps, and crossed-out entries tell you whether the maker actually lives by their stated standards or just talks about them.
A glossy brochure can claim a tolerance of ±0.005 mm, but the floor record reveals how often parts actually landed outside that window and what the maker did about it. Did they quietly ship them anyway? Did they rework and re-measure? The presence of detailed non-conformance reports isn't a red flag; it's evidence of a maker who doesn't hide their mistakes. A clean floor record with no deviations is more suspicious than one full of honest notes.
Over time, those records become a fingerprint. You can see whether the maker's quality improved after a supplier switch, whether machine maintenance was skipped before a big order, or whether the same defect keeps appearing every third batch. A sales pitch changes with the audience, but a floor record stays in the drawer and tells the truth.
The One Question About Oven Insulation That Reveals a Lot
Ask an oven salesperson how the cavity walls are insulated and you’ll quickly see who knows their product. The ones worth buying usually have a clear answer: a full wrap of high-density fiberglass or mineral wool around the baking chamber, not just a thin sheet tacked onto the back. That single detail tells you more than a dozen spec-sheet bullet points because it directly affects how evenly the oven holds temperature, how often the elements cycle on, and whether the outer panels stay safe to touch.
Cheaper ovens often skimp here, leaving gaps above the door or along the side walls. The result is a unit that works fine for a frozen pizza but struggles with anything that demands stable heat, like a slow braise or a delicate soufflé. If the answer you get is vague or the display model doesn’t have a cutaway, treat that as a warning sign. A well-insulated oven doesn’t need a marketing story; the design speaks for itself.
How to Spot a Builder That Truly Understands Carousel Timing
A builder who truly understands carousel timing won't slap a five-second default onto every slide. They'll ask about content density, reading speed, and whether the carousel even needs to move on its own. You'll notice it in the details: a pause when someone hovers, a gentle slowdown for longer text, and a hard stop after the last slide instead of an endless loop that ignores user intent.
Watch how the timing behaves on a real device, not just a preview. The carousel should wait for images to load before starting its countdown, and it should respect system settings for reduced motion without breaking the layout. If the builder can explain why a product shot deserves seven seconds while a brand statement gets four, you've found someone who treats timing as a design decision, not a technical afterthought.
The best builders also account for touch and keyboard interaction. A timed carousel that yanks control away mid-swipe or ignores a paused state on focus is a clear sign of shallow implementation. True understanding means the timing feels like a conversation—responsive, predictable, and easy to interrupt.
What Custom Mold Experience Actually Looks Like in Practice
Walk onto a production floor where custom molds are the norm, and the first thing you notice is how conversations change. Instead of debating whether a part can be made, teams talk about draft angles, gate placement, and how the polymer flows around a tricky undercut. There's no single mold experience—each project starts with a blank CAD file and a list of constraints that often contradict each other. One supplier might spend two days just running mold flow simulations to predict warpage before cutting steel. Another will hand-polish a cavity for eight hours because the customer's texture spec demands a matte finish that hides fingerprints. The real practice is messy, iterative, and rarely follows a straight line from quote to tooling.
What separates a frustrating project from a smooth one usually isn't the machine park—it's how the mold maker handles feedback loops. A good shop will send you a video of the first shot within minutes of the press cycling, not three days later with a formal report. They'll ask about your end-use environment before quoting, because they know a mold for a humid bathroom fixture needs different venting than one for a dry automotive clip. And when ejection marks show up on a visible surface, they don't just mirror polish the area; they might suggest moving the gate or adjusting pack pressure to eliminate the root cause. That level of ownership is hard to fake, and it's the part of custom mold work that no brochure ever captures.
The practical rhythm also includes a lot of waiting that no one talks about. Steel arrives late from the mill. A hot runner manifold fails a bench test. The customer changes a wall thickness after the core is already roughed. Experienced teams build buffer into their timelines without calling it buffer—they call it "engineering review" or "supplier coordination." Meanwhile, the mold itself gets broken in gradually: first a few dozen shots at slow cycle time, then hundreds to check dimensional stability, then finally a short production run with real resin and real operators. Only after that hand-off do you realize the custom mold experience wasn't just about making a cavity; it was about troubleshooting a thousand small decisions that never show up on the final invoice.
Support and Spare Parts Red Flags Once the Machine Is Yours
Once the machine is sitting on your floor, the support line becomes the real spec sheet. A surprising number of brands answer pre-sales calls in two rings but go silent after the invoice clears—emails bounce, the local tech they promised never materializes, and you're stuck explaining your problem to a chatbot that offers nothing but a ticket number. If you can't reach a human who knows the model within a day, treat that as a bigger red flag than any missing feature.
Spare parts will tell you more than the brochure ever did. Ask about a common wear item—a belt, blade, seal, or filter—and listen carefully to the answer. If the only source is a single warehouse across the border with a six-to-eight-week lead time, you don't own a machine; you own a countdown. Some manufacturers also require you to buy all consumables from them at inflated prices, which says a lot about how they view customer loyalty.
The warranty fine print is where the real gotchas hide. Look for clauses that exclude the parts most likely to fail after month six, or that require you to ship the entire unit back for diagnosis at your own expense. A company that actually supports its equipment will have local repair partners, realistic turnaround estimates, and a parts diagram they're willing to share—not a legal shield designed to make you give up and buy a replacement.
Weighing the True Cost of Changeover and Idle Time
Changeover and idle time rarely show up as a single line item on a profit-and-loss statement, yet their combined drag on output can quietly erase the gains from faster cycle times or cheaper materials. A press that sits still for forty minutes between jobs isn't just losing forty minutes of potential production; it's also tying up the crew, delaying downstream assembly, and pushing overtime into the weekend. When managers treat setup as a fixed annoyance rather than a variable cost, they miss the chance to recover capacity that's already been paid for.
The true cost becomes clearer when idle minutes are converted into labor hours, missed shipments, and the extra inventory needed to buffer against unreliable changeovers. For example, a packaging line that requires two hours to switch from one product to another may force the plant to run larger batches than customers actually need, inflating warehousing costs and increasing the risk of obsolescence. Meanwhile, operators standing by during a lengthy adjustment aren't free; their time is being spent without adding value, which raises the real cost per unit well above the standard rate.
Weighing these costs properly means looking beyond the stopwatch. A short setup that produces defects or requires rework is more expensive than a slightly longer one that starts cleanly. Smart teams measure changeover as a system—from the last good piece of the old job to the first good piece of the new one—and then compare that total against the cost of alternatives, such as dedicated lines, quick-release tooling, or staggered shifts. Only by accounting for labor, lost output, quality risk, and schedule disruption can a business decide whether reducing changeover time is truly worth the investment.
FAQ
Look for a partner who can talk about oven temperature uniformity, arm indexing accuracy, and mold mounting specifics without hesitating. Ask about past projects with similar part sizes and wall thickness requirements, and pay attention to whether they mention real production challenges like warpage or porosity rather than just listing features.
Heavier frames and better-insulated ovens tend to hold temperature more consistently and resist distortion over years of cycling. If a supplier avoids giving you structural weight or insulation details, that's often a warning sign because these directly affect cycle time and energy use.
You should get more than a phone number. Ask if they offer on-site commissioning, operator training, spare parts stocking, and remote troubleshooting. A solid partner will also schedule follow-up visits or check-ins after the line is running, not disappear once payment clears.
There is no universal rule, but a specialist often has deeper knowledge of carousel timing, oven airflow, and mold changing sequences. If you choose a generalist, make sure they can show several working carousel installations and connect you with customers who run similar products.
Request detailed video walkthroughs of their assembly floor, ask for references from at least two customers with comparable output, and check whether their documentation includes actual cycle time data for your part family. A confident maker will share this without making you sign a purchase agreement first.
Bring drawings or dimensions of your existing molds and ask how the carousel arms handle different offsets and mounting patterns. Inquire how long a typical mold change takes with their tooling and whether quick-change features are standard or optional. Their answers reveal how much they understand your daily operation.
Look beyond the quote. Ask for estimated energy consumption per cycle, expected service life of major components like bearings and burners, and typical maintenance intervals. A slightly higher upfront price often pays back quickly if the oven insulation and drive system reduce fuel and downtime.
Conclusion
When you're standing in a maker's facility evaluating a stationary oven carousel rotomolding machine, the first thing to look at isn't the brochure or the polished demo—it's how many carousel stations are actually running, and what the operators do when a cycle hiccups. A builder with a long floor record will have machines at different stages of a run, molds being swapped, and a maintenance log that gets dirtied daily. Ask them pointedly about oven insulation: do they specify the kiln lining thickness in the hot spots, or do they hand you a generic spec sheet? The answer tells you whether they've ever had to rebalance a carriage after uneven heat warped a mold arm. You also want to see evidence of custom mold work that goes beyond drilling a few vents—ask to walk through a recent job where a client's part kept bridging or thinning at the corners. The maker who can describe how they adjusted arm speed, dwell angle, and cooling air for that specific geometry is worth far more than one who quotes cycle times from a catalog.
After the install, the real costs show up in changeover and idle time. A sharp builder will have designed the carousel index so a single operator can swap a mold without calling for a crane, and they'll stock the wear plates and burner nozzles locally instead of making you wait three weeks for an overseas shipment. Red flags include a support line that routes to voicemail during your first month, or a spare parts list that's just the machine's exploded diagram without a recommended on-hand quantity. Ask current customers how long their line sat idle after a relay failure—not how fast it ran on day one. Weighing those hidden hours against a slightly lower purchase price usually reveals why the cheapest bidder often ends up costing more in lost production.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com